
Bronze bushings for construction and mining machinery
Pin joints on earthmoving and mining machines see shock, edge loading, mud and long intervals between greasing, and a worn pin costs many times a worn bush. Cast bronze bushes in C86300, aluminium bronze and C93200 protect the pin, embed the grit and can be greased back to life; replacing worn factory steel bushes with bronze is a common repair wherever the joint can be greased.
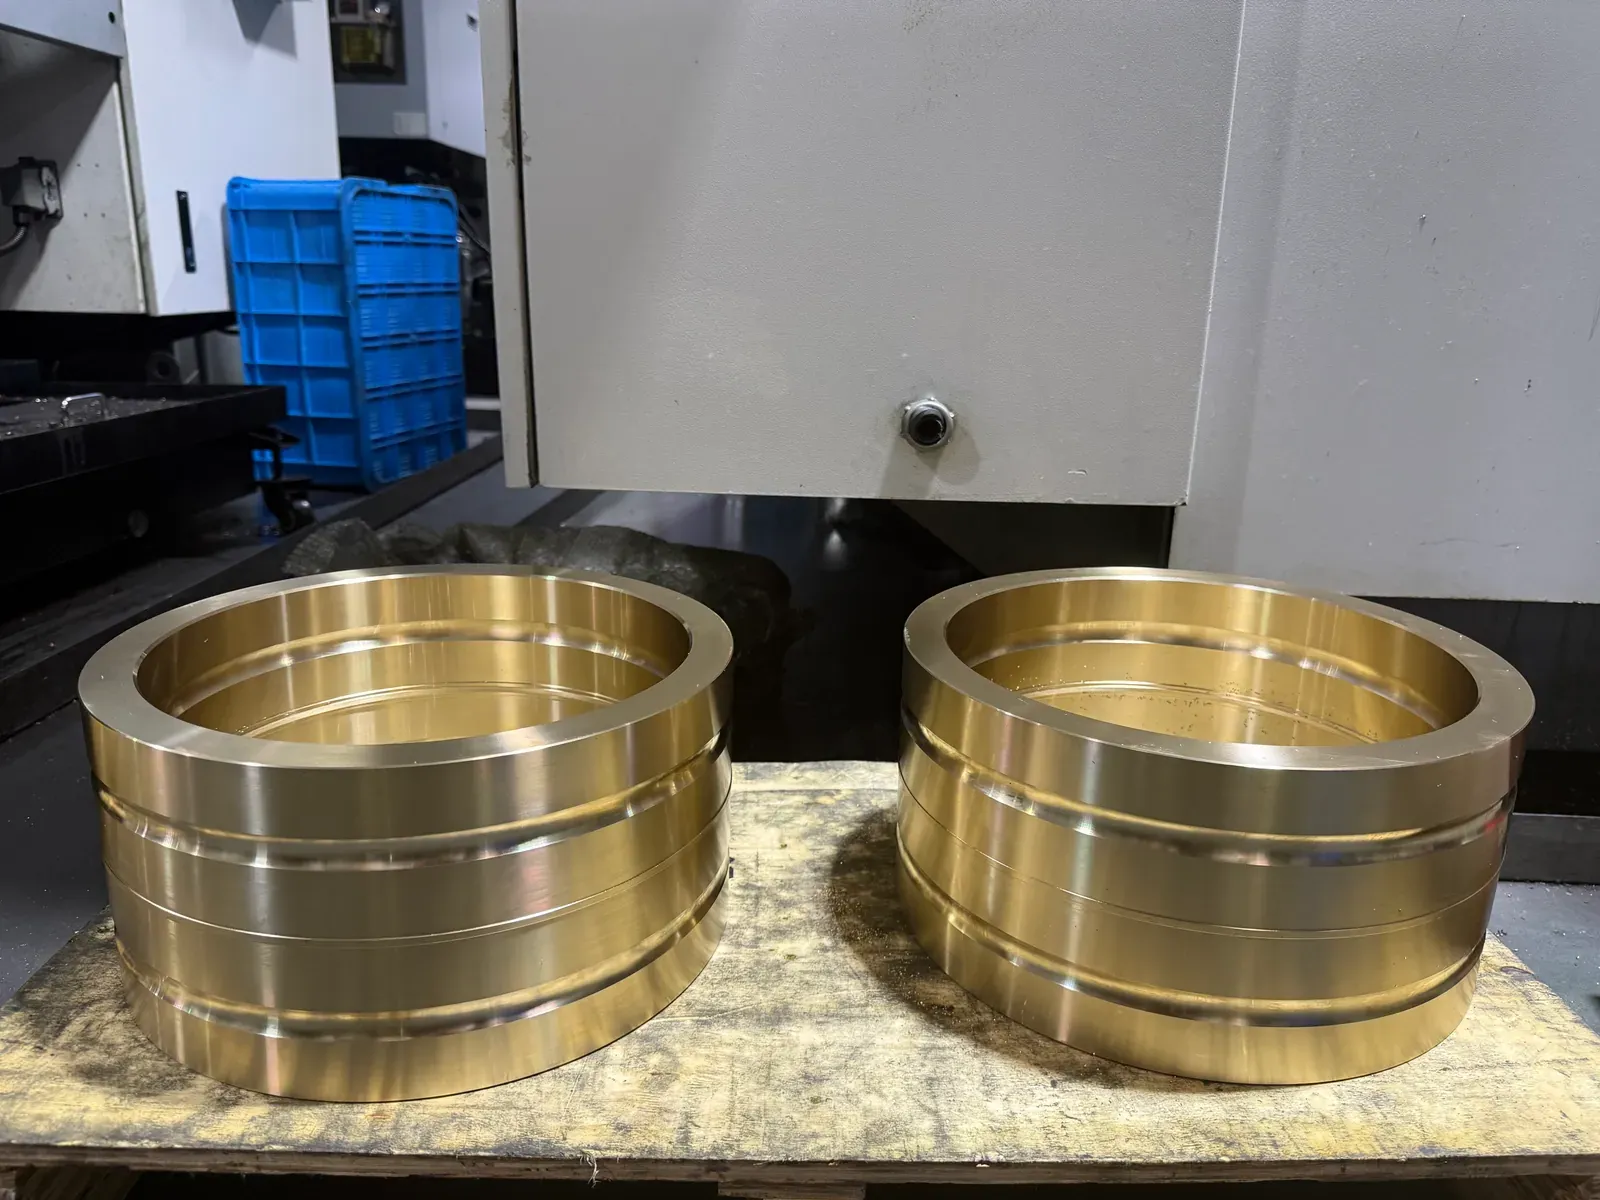
Where a pin oscillates under high load in dirt, a machined cast bronze bush is the bearing: it carries 25 N/mm² dynamic and 45 N/mm² static, takes shock without cracking, embeds sand rather than scoring the hardened pin, and is re-greased through the pattern of grooves. The alloy is chosen by load and shock, the groove pattern by movement, and the size is whatever the drawing or the worn part says.
- Boom, stick and bucket pins: C86300 or C95400, Ø50 – 200 mm, figure-eight grooves
- Loader linkage, tipper and crane pivots: C93200 or C95400, Ø30 – 150 mm
- Slew rings and sheaves: thrust washers and large flanged bushes to Ø1000 mm
- Crusher eccentric bushes and thrust plates: aluminium bronze and C86300, machined to drawing
- Replacement bushes from the worn part's dimensions – no MOQ, samples in 3 – 5 days
Where bronze bushings are used on the machine
| Position | Movement | Load | Contamination | Alloy | Form and grooves |
|---|---|---|---|---|---|
| Boom / stick / bucket pins | oscillating ±30 – 90° | very high, shock, edge loading | mud, sand, water | C86300 · C95400 | sleeve or flanged, G4 / G5, seals in housing |
| Loader articulation and lift arms | oscillating | high, shock | dust | C95400 · C93200 | sleeve, G4, oil hole to nipple |
| Dozer equaliser bar, track adjusters | small oscillation | very high | dust, dry | C86300 | thick-wall sleeve, G2 or G8 |
| Crane sheaves and luffing pivots | rotating slow / oscillating | high | weather | C93200 · C95400 | flanged sleeve, G3 / G6 for sheaves |
| Slew bearings and turntables | rotating slow | axial + radial | weather | C93200 · CuSn12 | thrust washers G7, large sleeves |
| Crusher eccentrics, thrust plates | rotating slow, heavy | extreme, shock | rock dust | C86300 · C95500 | thick-wall to Ø1000, to drawing |
| Vibrating screen suspensions, feeders | oscillating fast | medium, vibration | dust | C93200 · C95400 | flanged, G2 |
| Hydraulic cylinder eye bushes | oscillating | high, shock | dust, water | C86300 · C93200 | sleeve, G2 / G4 |
Send pin diameter, bore and length plus a photo of the worn bush – we quote in 12 hours.
Bronze or hardened steel bushing for pin joints?
Factory joints on many excavators use hardened steel bushes on hardened pins – cheap in volume and acceptable while the central lubrication works. What are excavator bushings made of? Both, and the choice is a maintenance decision:
| Criterion | Cast bronze bush | Hardened steel bush |
|---|---|---|
| Greasing lapses | runs on residue for a while, embeds grit | steel-on-steel galls and seizes |
| Pin protection | the bush wears, the expensive pin survives | both wear; pin often scrapped with the bush |
| Shock and misalignment | conforms, no cracking | hard but brittle edge loading |
| Wear life with grease | long; can be re-bored and re-greased | long while lubricated; short after |
| Replacement | press out, press in; to any dimension, no MOQ | OEM part or hardened sleeve to order |
| Cannot be greased at all | not suitable – choose graphite-plugged bronze | not suitable either |
Recommended alloys
C86300 / SAE 430B for the heaviest shock – boom and bucket pins, crusher parts, dozer equalisers – on a hardened, ground pin (300 HB minimum, typically 42CrMo4 / 4140 quenched and tempered or induction hardened) with EP grease. C95400 / C95500 aluminium bronze for heavy load with water and mud, and where the pin is hardened: loader linkages, crane pivots, cylinder eyes. C93200 / SAE 660 for general pivots at moderate load and for machines whose pins are not hardened – it forgives the shaft and the grease schedule. Cast bronze bushes are not offered where the joint can never be greased; that is a graphite-plugged bush.
Grooves, seals and relubrication in dust
Figure-eight (G4) or double figure-eight (G5) grooves distribute grease around an oscillating pin and wipe fresh grease under the load with each stroke; the oil hole is aligned with the housing nipple before pressing. Dust seals in the housing ends – lip seals or O-rings in grooves – keep the mud out and the grease in. Grease daily to weekly per the machine maker; purge until clean grease shows at the seal. Where the interval cannot be kept, specify grease pockets (G8) for reservoir or move to a self-lubricating type.
Sizes and replacement parts
Pin bushes run from Ø30 to Ø200 mm on most machines, with thrust washers and slew bushes to Ø1000 mm. Replacement parts are machined to the drawing or to the dimensions you measure from the old bush and the housing – bore at the unworn end, outside diameter or housing bore, length, flange, groove pattern – and to the pin diameter for the clearance. Metric and inch. One piece or a batch, samples in 3 – 5 days, raw-material certificate with the delivery.
Alloy by position
| Alloy | Choose for | Pin | Notes |
|---|---|---|---|
| C86300 / SAE 430B | boom and bucket pins, crushers, equalisers | hardened 300 HB+, ground | highest strength, needs EP grease |
| C95400 · C95500 | loader and crane pivots, wet and muddy joints, cylinder eyes | hardened, Ra ≤ 0.8 | seawater and heat resistant |
| C93200 / SAE 660 | general pivots, unhardened pins, sheaves | plain steel acceptable | best embeddability, lowest cost |
| CuSn12 | slow rotating sheaves and slew rings with oil | hardened | higher wear resistance, lead-free |
Parts we machine for this sector
Type-level list of the parts that come through the shop for earthmoving and mining machines:
- Boom, stick and bucket pin bushes Ø50 – 200 mm, C86300 and C95400, with figure-eight grooves and oil holes
- Flanged linkage bushes for loaders and tippers, C93200 and C95400
- Large flanged sleeves and rings for crane sheaves and slew bearings, to Ø1000 mm
- Thrust washers with radial grooves for turntables, C93200 and CuSn12
- Crusher eccentric and thrust bushes to customer drawings, aluminium bronze and C86300
- Hydraulic cylinder eye bushes, C86300 / C93200
What to send for a quote
For a replacement bush or a drawing part:
- Pin diameter and bore or the old bush's bore at the unworn end
- Outside diameter (or housing bore) and length; flange if any
- Alloy or duty (load, shock, greasing interval)
- Groove pattern (G-code) and oil hole position, or "as the sample"
- Quantity and whether a sample is wanted first
- A photo of the worn part helps, a drawing is best
Frequently asked questions
What bronze is used for excavator bushings?
C86300 manganese bronze for the heaviest boom and bucket pins, C95400 aluminium bronze for heavy loaded and wet joints, C93200 / SAE 660 for general pivots and unhardened pins. All need grease; the pin should be hardened for C86300 and aluminium bronze.
Can I replace steel bushings with bronze?
Yes, in the same housing and pin sizes, as long as the joint is greased: bronze protects the pin and survives lapses in greasing better than steel-on-steel. We machine the bush to the housing and pin dimensions with the correct press fit and clearance.
How often should pin bushings be greased?
Follow the machine maker's schedule – daily to weekly for working pins – and purge until clean grease appears. Halve the interval in water, mud or heat. A bronze bush must never run on dried residue.
Do you make bushings for Caterpillar or Komatsu part numbers?
We machine bushes to the dimensions and drawing you provide for any machine; we do not sell by OEM part number or brand. Send the measured old part or the drawing and we quote the replacement.
Do you sell used bushings?
No – every bush is newly machined from cast bronze stock, with a raw-material certificate.
Replacement bushings to your measurements – no MOQ
Send pin diameter, bore and length plus a photo of the worn bush. Quote in 12 hours, samples in 3 – 5 days.